Hydraulic Servo
HPS1250
X Axis Traverse Speed 75 m/min
Y Axis Traverse Speed 60 m/min
Working Tables Size Brush
Features
PRECISION AND SPEED EFFICIENCY
PROGRAMMABLE PUNCH/ RAM STROKE DISTANCE
Advanced German made Schneider Hydraulic Servo system with pressure valve to precisely control the speed, volume and pressure of oil flow.
To control RAM stroke distance on both ends, hence the height and depth of each punch becomes programmable with 0.1mm accuracy faster punching speed.
HPS1250X is with 2490 ± 10mm X-Axis.
Specifications
| Item | Unit | HPS1250 |
|---|---|---|
| Punching Capacity | Ton | 20 |
| X axis Travel Length | mm | 1250±10 |
| Y axis Travel Length | mm | 1250±10 |
| Max Sheet Size | mm | 1250x2500 |
| Max Sheet Thickness | mm | 6.35 |
| Max.Sheet Weight | kg | 110 |
| X Axis Traverse Speed | m/min | 75 |
| Y Axis Traverse Speed | m/min | 60 |
| Max Traverse Speed | m/min | 96 |
| Punching Speed at 25mm pitch | hist/min | 360 |
| 25mm Between Holes | ||
| Nibbling Speed (stroke length 4mm, pitch 1mm) | hits/min. | 600 |
| Tools Type | Thick turret | |
| Max Punching Diameter | mm | 88.9 |
| Number of Tool Stations | 34 | |
| Numer of Auto Index Stations | 2/(BType) | |
| Turret Rotating Speed | rpm | 40 |
| Auto Index Rotating Speed | rpm | 50 |
| Ram Stroke Distance | mm | 0-31(Hydraulic servo axis) |
| Working Tables Size | Brush | |
| Number of Sheet Clamps | 2 | |
| Power Supply | KVA | 25 |
| Air Supply | NL/min | 250 |
| Oil Tank Volume | L | 350 |
| Air Pressure | bar | 5 |
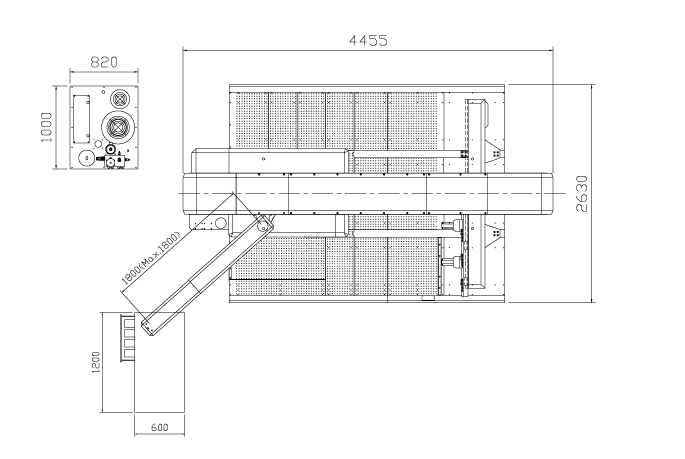
| Machine Size | mm | 4455x2630x2100 |
| Net Weight (apporx) | kg | 11000 |
| Size of Control Cabinet | mm | 1200x600x1900 |
| CNC Controller | FANUC Oi-PF | |
| Number of Controllable Axis | 5+1 | |
| Memory | KB | 512 |
| Serial Interface | RS232 | |
| Punching Accuracy | mm | ±0.1 |
Specifications are subjects to change without prior notice. Acceleration / deceleration rate of X / Y-axis are dependent on weight of materials. Punch speed depends on processing conditions, stroke length, acceleration / deceleration of axes speeds.
Station Arrangement
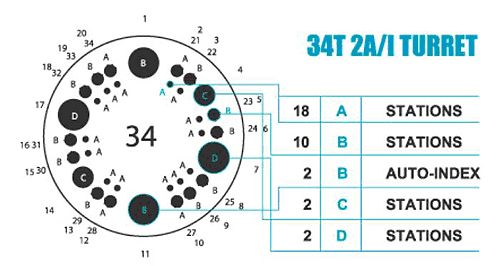
| Atype (1/2") MAX diameter 12.75mm | 18 (14 accept shaped tools) |
| Btype (1-1/4") MAX diameter 31.75mm | 10 (10 accept shaped tools) |
| Btype (1-1/4") MAX diameter 31.75mm | 2 AUTO. INDEX |
| Ctype (2") MAX diameter 50.8mm | 2 (2 accept shaped tools) |
| Dtype (3-1/2") MAX diameter 88.9mm | 2 ( 2 accept shaped tools ) |
Layout
FAQ
Not necessarily. The process of automating an entire factory and production line inherently involves a gradual integration—starting with the automation of individual machines and progressing to the integration of automated warehousing and management software—so planning can be done in phases based on on-site conditions.
It can integrate sheet metal processing equipment such as laser cutters, CNC press brakes, turret-type punch presses, welding equipment, and automatic multi-angle bending centers.
In addition to the processing equipment itself, it also includes automatic loading and unloading systems, automatic coil feeding systems, storage racks, management and control software, monitoring interfaces, and material flow scheduling systems.
Typically, sheet metal factories facing labor shortages, lengthy material handling times, frequent line changes, difficult-to-manage scheduling, or those seeking to extend continuous processing time.
Standalone machine automation is not sufficient; integration with automated warehousing and related management and control software is also required to achieve production automation control and Industry 4.0 goals.
Still unsure if an automated production line is right for you?
Tell us about your current equipment setup, bottleneck processes, and production capacity goals, and Tailift will help you evaluate the most suitable sheet metal automation solution!
[Inquire About Sheet Metal Automation Solutions Now]